
Filling technology selection
Filling Machine Capacity Is More Than BPH
Required nominal BPH = target saleable bottles per day / (planned production hours per day × combined operating efficiency). For example, 60,000 bottles over 8 hours at an assumed 80% efficiency requires 9,375 BPH. Use the calculator and worked example below, then confirm that rate with your beverage, bottle, cap and connected equipment.
Send Target and Current OutputCapacity planning worksheet
Calculate Required Bottles per Hour
Use your daily accepted-bottle target, planned production time and an explicit efficiency assumption. The calculation runs in your browser; it sends no inquiry and stores no input.
Planning requirement:
60,000 bottles / (8 hours × 80% efficiency) = 9,375 BPH, rounded up to a whole bottle.
- Nominal bottles per minute
- 156.25 BPM
- Average saleable bottles per planned hour
- 7,500 bottles/h
- Nominal filled-volume rate
- 4,687.5 L/h at 500 ml
This is a planning calculation, not guaranteed equipment performance or a final model selection. Combined efficiency includes availability, running-speed and quality losses once. Keep excluded breaks out of planned hours and do not deduct the same downtime twice. The volume result is not a utility, pump or CIP sizing calculation.
Request a machine review using your bottle and calculated output
Machine selection and configuration
Three output numbers
Rated speed
A model or design reference under stated conditions.
Sustainable output
A repeatedly achievable rate with the confirmed beverage, package and line conditions.
Saleable output
Accepted product after rejects, stops, changeovers and losses.
Machine selection and configuration
Capacity inputs
- Reference bottle size and drawing
- Beverage temperature, viscosity and carbonation
- Fill accuracy or level basis
- Changeover pattern and planned downtime
- Upstream supply stability
- Downstream accumulation and packing limits
- Operator and maintenance assumptions
Machine selection and configuration
Worked example: 60,000 saleable bottles per day
Illustrative planning assumptions, not a machine performance promise. Use one consistent production-time denominator.
| Input or result | Example | Meaning |
|---|---|---|
| Daily sales-ready target | 60,000 bottles | Good, accepted bottles; excludes rejects |
| Planned production time | 8 hours | Hours after excluded breaks; do not deduct the same stop again in efficiency |
| Combined operating efficiency | 80% assumed | Accounts once for availability, running-speed loss and quality loss |
| Required nominal machine rate | 60,000 / (8 × 0.80) = 9,375 BPH | A screening requirement on the actual reference bottle, not a model recommendation |
| Bottles per minute | 9,375 / 60 = 156.25 BPM | Useful when comparing conveyors, labelers and inspection equipment |
| 500 ml reference-volume rate | 9,375 × 0.5 = 4,687.5 L/h | Nominal filled volume only; not a pump, treatment or CIP design rating |
Machine selection and configuration
Capacity review example
| Question | Incomplete answer | Useful answer |
|---|---|---|
| Target output | 10,000 BPH | 10,000 BPH sustainable on 500 ml PET still water after agreed acceptance test |
| Other sizes | Also 1.5 L | State required rate and changeover frequency for each size |
| Line constraint | None | Document blower, labeler, packer and conveyor limits |
Machine selection and configuration
Avoid double-counting downtime and rejects
Build efficiency from one time basis
If measured availability is 90%, performance is 95% and quality is 99%, their product is 84.645%. Use 0.84645 as the combined factor. These are example assumptions, not industry averages.
Keep excluded breaks outside the denominator
If the planned hours already exclude a break or sanitation window, do not deduct it again through availability. Changeovers, stops and rejects must each appear only once in the calculation.
Check every SKU separately
A 1.5 L rate cannot be inferred by dividing a 500 ml catalog speed by three. Valve flow, fill time, container handling and closure performance can set different limits. Request an output matrix for each bottle and beverage.
Test the slowest connected operation
A filler cannot deliver its full rate when bottle supply, product preparation or packing is slower. Compare all machines on the same bottle and operating assumptions; a buffer can absorb short stops but cannot remove a sustained capacity gap.
Machine selection and configuration
Turn the calculation into a testable specification
Filling machine technical specification
Record product condition, one reference bottle, utilities and the required output for each SKU.
Filling machine technical specificationFactory acceptance test checklist
Agree the test duration, count method, stop log and quality criteria before testing the proposed speed.
Factory acceptance test checklistFilling machine quotation scope
Compare offers only when their output basis, included interfaces and acceptance conditions match.
Filling machine quotation scopeCatalog equipment evidence
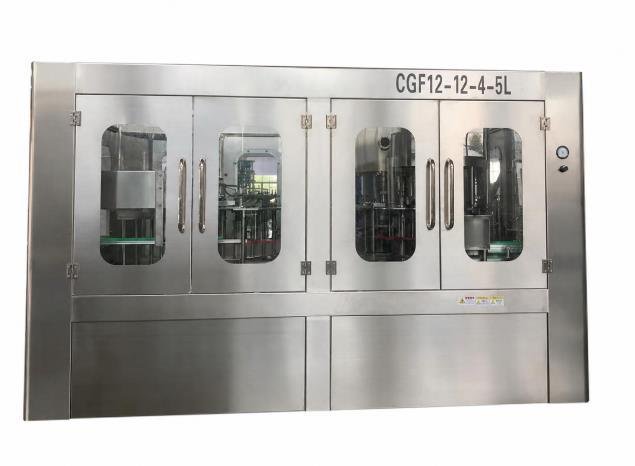
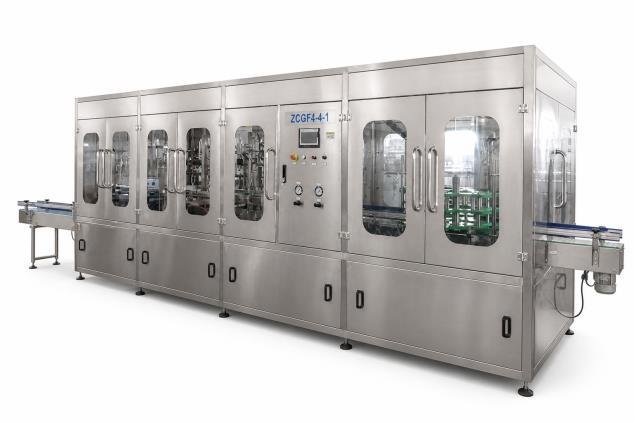
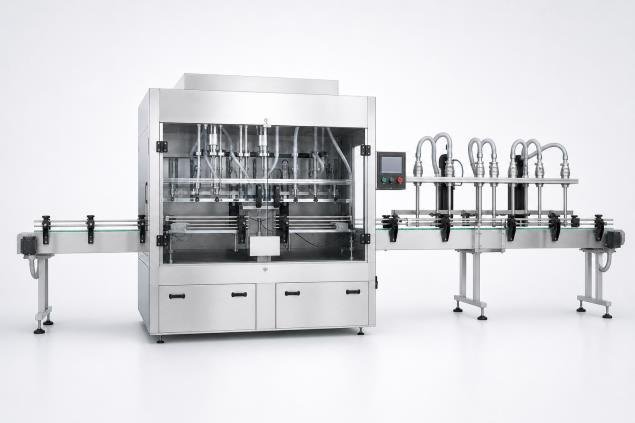
Machine Architecture Changes the Capacity Discussion
Compare rotary, linear and piston-filling arrangements only after product, package, changeover and sustainable-output conditions are aligned.
Engineering decision guide
Continue the buyer decision path
Use these pages in sequence to understand, compare, plan, choose and prepare a project-specific request.
-
Beverage Filling Machines
Compare filling machine families by beverage behavior, filling basis, package handling and the interfaces required around the filler.
-
Filling Technology Comparison
Compare gravity, hot-fill and isobaric routes against the same product, package, acceptance and cleaning facts.
-
Filling Machine Capacity Guide
Define required saleable output by bottle size, product, shift pattern and planned efficiency before comparing nominal machine rates.
-
Filling Machine Selector
Generate a preliminary technology route from beverage, process, package and output inputs, then verify open assumptions with an engineer.
-
Request a Filling Machine Recommendation
Send a structured machine brief with the known product, package, output, site and project facts, while marking unknowns openly.
Buyer questions
Frequently asked questions
What is the difference between rated and sustainable output?
Rated speed is a stated machine reference; sustainable output is the repeatedly achievable rate under the confirmed product, package, changeover and connected-line conditions.
Why is a 500 ml BPH value not valid for every bottle?
Bottle height, diameter, stability, fill volume, cap, product behavior and transfer conditions can change cycle time and losses. Each required format needs its own accepted output basis.
Should filling-machine capacity equal the required saleable line output?
Not automatically. The project must account for changeovers, planned stops, rejects, product transitions and upstream or downstream constraints before setting the machine rating and acceptance target.
How do I calculate the BPH needed for my daily bottle target?
Divide target saleable bottles per day by planned production hours multiplied by combined operating efficiency as a decimal. For 60,000 bottles, 8 hours and an assumed 80% efficiency, 60,000 / (8 × 0.80) = 9,375 BPH. Validate the selected machine on the actual product and bottle.
Last reviewed:
Next machine-selection action
State the output with its operating basis.
Send the reference package, required sustainable rate, shifts, changeovers and connected-equipment constraints.